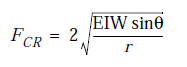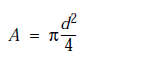Showing posts with label bit hydraulics. Show all posts

Wednesday, 3 February 2016

The E*C TRAK Torque and Drag Module

The E*C TRAK Torque and Drag Module
This program, developed at the Drilling Research Center in Celle,
Germany, is used to calculate torque and drag when a friction factor
(coefficient of sliding friction) is known or estimated. It will calculate the
friction factor when either torque or hookload is known.
Software accuracy has been verified against actual field data, with inputs
and outputs handled in user selected units.
General Uses
The program may be used to:
• Optimize well path design for minimum torque and drag
• Analyze problems either current or post-well
• Determine drillstring design limitations
• Determine rig size requirements
Inputs Required
• Drillstring component data (OD, ID, tool joint, and material
composition)
• Survey data (actual or planned)
• Friction factor(s) or actual hookload or torque values (for friction
factor calculation)
Outputs
Information concerning loads, torques and stresses are calculated for
discrete points in the drillstring from rotary table to the bit. These values
are output in both tabular (summary or detailed) and graphical formats:
• Drag load (pick-up or slack-off)
• Pick up load
• Slackoff load
• Rotating off bottom load
• Drilling load
• Rotating off bottom torque
• Rotary torque (drilling and off-bottom)
• Maximum allowable hook load (at minimum yield)
• Drillstring weight (in air)
• Bit to neutral point distance drillstring twist
• Drillstring twist
• Axial stress
• Torsional stress
• Bending stress
• Total equivalent stress

Tuesday, 2 February 2016

Calculating BHA Weight With Drill Pipe In Compression - Summary

Calculating BHA Weight With Drill Pipe In Compression
Summary

• When drilling vertical wells, ordinary drill pipe must NEVER be run
in compression, in any hole size. Therefore, sufficient BHA weight
must be used to provide all the desired weight on bit with an
acceptable safety margin, except at higher inclinations.
• In large hole sizes (16-inch or greater) drill pipe should not be run in
compression.
• In smaller hole sizes on high-angle wells (over 45°), drill pipe may be
run in compression to contribute to the weight on bit, provided the
maximum compressive load is less than the critical buckling force.
This critical buckling force is the minimum compressive force which
will cause sinusoidal buckling of the drill pipe.
• A safety margin of at least 10% should be used in the calculation to
allow for some drag (friction) in the hole. However, axial drag is not a
major factor when assemblies are rotated.
The majority of the preceding discussion concerned rotary assemblies.
However, it would also apply to steerable motor systems used in the
rotary mode, with only minimal oriented drilling anticipated, the
required BHA weight could be calculated the same way. If a
significant amount of oriented drilling was likely, then the drag in the
hole should be evaluated using Torque and Drag computer programs.
In this type of situation, a proper engineering analysis of BHA weight
requirements is advised.

BHA Weight For Steerable Motor Assemblies

BHA Weight For Steerable Motor Assemblies


In practice, BHA weight for steerable assemblies on typical directional
wells is not a problem for the following reasons.
• The WOB is usually fairly low, especially when a PDC bit is used.
• When the drillstring is not rotated, the drill pipe is not subjected to the
cyclical stresses which occur during rotary drilling. Therefore,
sinusoidal buckling can be tolerated when there is no rotation of the
drillstring. Helical buckling however, must be avoided.
Helical buckling occurs at 1.41 FCR, where FCR is the compressive force
at which sinusoidal buckling occurs.
Therefore, if BHA weight requirements are evaluated as for rotary drilling,
the results should be valid for steerable systems in the oriented mode
except for unusual well paths which create exceptionally high values of
axial drag.

Monday, 1 February 2016

BHA Requirements When The Drillstring Is Not Rotated

BHA Requirements When The Drillstring Is Not Rotated


As stated earlier, when the drillstring is rotated, the component of sliding
friction (drag) is small and may be compensated for by using a safety factor
in BHA weight calculations. Drillstring friction for rotary assemblies will
mainly affect torque values. When the drillstring is not rotated (a steerable
motor system in the oriented mode) axial drag can become very significant
and drillstring friction should be evaluated.
A proper analysis of drillstring friction is more complex and must take into
account a number of factors, including wellbore curvature.

Calculating BHA Weight With Drill Pipe In Compression

Calculating BHA Weight With Drill Pipe In Compression
This means that on high-angle wells in small hole sizes, a fraction of the
weight on bit can safely be provided by having drill pipe in compression. It
is suggested that 90% of the critical buckling force be used as the
maximum contribution to the weight on bit from ordinary drill pipe.
Denoting the total air weight of the BHA by WBHA the weight on bit by
WBIT and the critical buckling load by FCR, we have:

Continuing example 4.5, recalculate the weight of the BHA required
(assuming some drill pipe is to be run in compression).
Suppose we are using New 5-inch Grade E drill pipe with 4.5-inch IF
connections.
Referring to the table for 5-inch drill pipe in a 12.25-inch hole, we see that
the critical buckling load at 60° inclination is approximately 26,000 lbs.
Our formula then gives:

Thus, a total air weight of 82,000 lbs is required. This is much more
feasible than the value of 138,000 lbs which was previously calculated.

Calculating Critical Buckling Force

Calculating Critical Buckling Force

Calculate the critical buckling load for 4.5-inch grade E drill pipe with a
nominal weight of 16.6 lb/ft (approximate weight 17.98 lb/ft; tool joint OD
6.375 inches: from API RP7G, Table 2.10) in an 8.5-inch hole at 50°
inclination.
1. Young's modulus, E, for steel is 29 x 10 psi


4.5-inch drill pipe with a nominal weight of 16.6 lbs/ft has an ID
of 3.826 inches. This information can be found under “New Drill
Pipe Dimensional Data” in the API RP-7G.


3. The approximate air weights for different sizes of drill pipe can
also be found in the API RP-7G.
Air weight = 17.98 lb/ft = 1.498 lb/in


Critical Buckling Force = 30,769 lbs

Running Drill Pipe In Compression

Running Drill Pipe In Compression


Example

Prior to drilling a 12.25-inch tangent section in a hard formation using an
insert bit, the directional driller estimates that they expect to use 50,000 lbs
WOB. The hole inclination is 60° and the mud density is 11 ppg.
What air weight of BHA is required if we are to avoid running any drill
pipe in compression? Use a 15% safety margin.


This is roughly the weight of ten stands of 8-inch drill collars, or
attentively, six stands of 8-inch collars plus 44 joints of HWDP!
This is just not practical! It would be a long, stiff and expensive BHA.


Critical Buckling Force
Dawson and Paslay developed the following formula for critical buckling
force in drill pipe.


where E is Young's modulus.
I is axial moment of inertia.
W is buoyed weight per unit length.
q is borehole inclination.
r is radial clearance between the pipe tool joint and the
borehole wall.
If the compressive load reaches the FCR, then sinusoidal buckling occurs.
This sinusoidal buckling formula can be used to develop graphs and tables
(see pages 4-18 through 4-23). If the compressive load at a given
inclination lies below the graph, then the drill pipe will not buckle. The
reason that pipe in an inclined hole is so resistant to buckling is that the
hole is supporting and constraining the pipe throughout its length. The low
side of the hole tends to form a trough that resists even a slight
displacement of the pipe from its initial straight configuration.
The graphs and tables provided in this section are for specific pipe/hole
configurations and may be used to look up the critical buckling force. The
following example illustrates how to calculate the critical buckling load.

Required BHA Weight For Rotary Assemblies

Required BHA Weight For Rotary Assemblies
When two contacting surfaces (i.e drillpipe and the borehole wall) are in
relative motion, the direction of the frictional sliding force on each surface
will act along a line of relative motion and in the opposite direction to its
motion. Therefore, when a BHA is rotated, most of the frictional forces
will act circumferentially to oppose rotation (torque), with only a small
component acting along the borehole (drag).
Measurements of downhole WOB by MWD tools has confirmed that when
the BHA is rotated there is only a small reduction in WOB due to drag.
This reduction is usually compensated for by using a “safety factor”.
Consider a short element of the BHA which has a weight “W” (see
following figure). Neglecting drag in the hole:
Effective weight in mud = W (BF)
Component of weight acting along borehole = W (BF) cosq
... where Q is the borehole inclination
Extending this discussion to the whole BHA,
WBIT = WBHA (BF) cosq
... where WBHA is the total air weight of the BHA and WBIT is the weight
on bit.
Therefore, if no drill pipe is to be run in compression

BHA Weight & Weight-On-Bit

BHA Weight & Weight-On-Bit

One important consideration in designing the BHA is determining the
number of drill collars and heavy-weight pipe required to provide the
desired weight-on-bit. When drilling vertical wells, standard practice is to
avoid putting ordinary drill pipe into compression (recommended by
Lubinski in 1950). This is achieved by making sure that the “buoyed
weight” of the drill collars and heavy-weight pipe exceed the maximum
weight-on-bit. This practice has also been adopted on low inclination,
directionally drilled wells.
In other types of directional wells, it must be remembered that since gravity
acts vertically, only the weight of the “along-hole” component of the BHA
elements will contribute to the weight-on-bit. The problem this creates is
that if high WOB is required when drilling a high inclination borehole, a
long (and expensive) BHA would be needed to prevent putting the drillpipe
into compression. However, for these high inclination wells, it is common
practice to use about the same BHA weight as used on low inclination
wells.
On highly deviated wells, operators have been running drillpipe in
compression for years. Analysis of drillpipe buckling in inclined wells, by
a number of researchers (most notably Dawson and Paslay), has shown that
drillpipe can tolerate significant levels of compression in small diameter,
high inclination boreholes. This is because of the support provided by the
“low-side” of the borehole.
Drillpipe is always run in compression in horizontal wells, without
apparently causing damage to the drillpipe.

Saturday, 30 January 2016

Bit Technology- Cutting Structures - Tungsten Carbide Cutting Structures

Tungsten Carbide Cutting Structures


Since most of the basic design features of the mill tooth cuttings structures
have been incorporated into insert bits, the main variations occur in insert
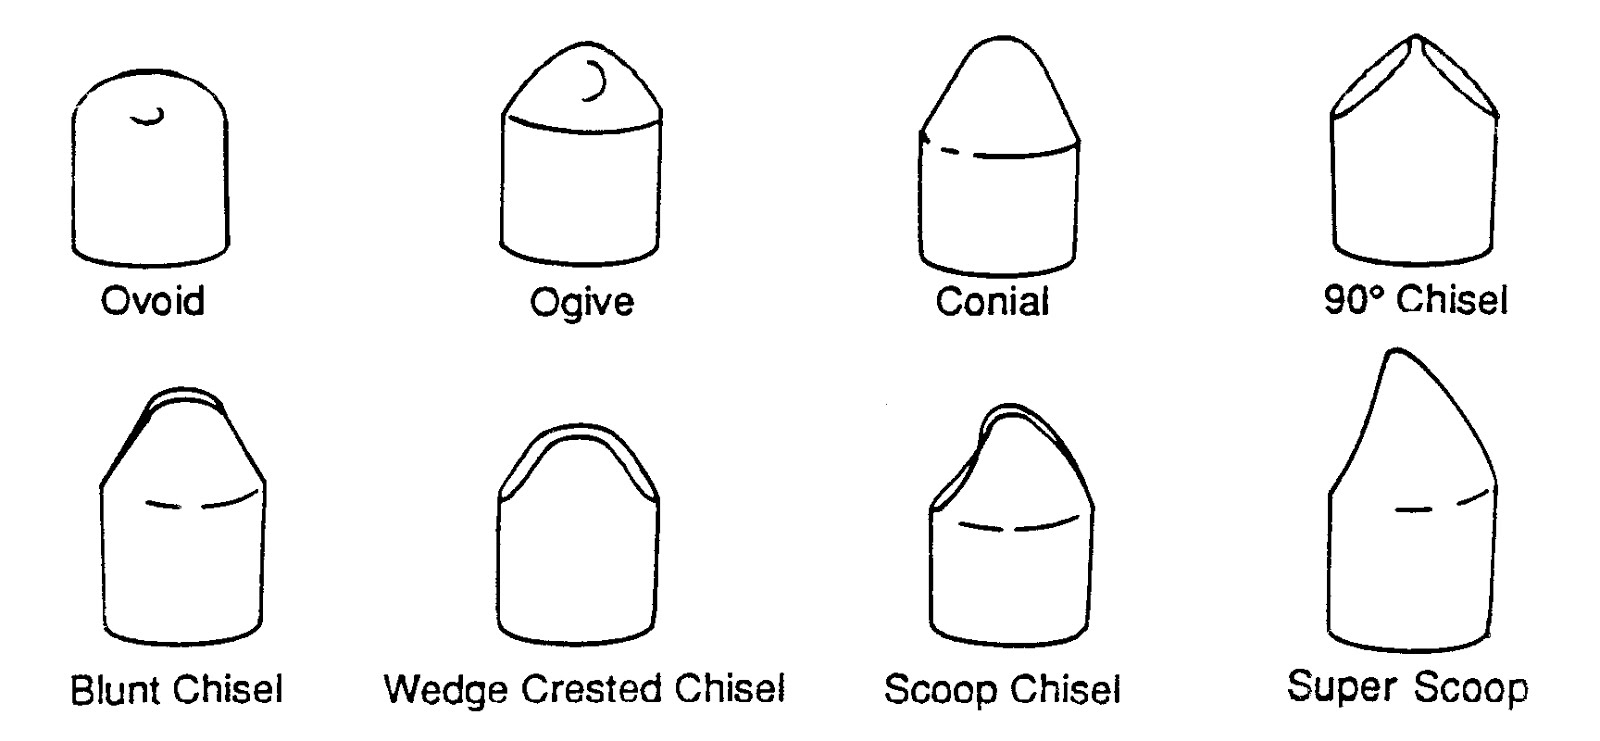
shape (Figure 3-5).


Figure 3-5: Tungsten Carbide Tooth Shapes
Historical shapes of milled teeth have built up a mystique about insert tooth
shape. Many people in the oil field thought that chisel shaped teeth
significantly affected the drill rate in all formations. This was because early
drilling practices used light bit weights, causing the relatively sharp chisel
shaped inserts to have a higher unit loading on the formation, hence faster
drill rates. When heavier bit weights are used, it tends to nullify the
advantage of the chisel shape. Even the steel milled teeth break down under
heavy weights. In fact, most bits drill 75% of the hole in a 1/2 to 3/4 dull
condition. With this in mind, many “blunt” insert tooth designs were made,
and seem to drill efficiently. Nowadays, most insert teeth have this blunt,
conical shape.

Bit Technology- Circulation Systems

Circulation Systems


The first hydraulic features incorporated into drilling tools dated back to
the original use of hollow drillpipe with direct circulation of drilling fluids.
As the first fishtail bits became popular, around the turn of the century,
circulation though water courses was used for the first time. The first
rolling cutter rock bits of 1909 introduced a central water course system
which directed fluid discharge towards the cutters.
In 1942, rock bits with jet nozzles were introduced to the oil industry. The
“jet bit” concept is considered to be the major hydraulic design
improvement in drill bits and remains state-of-the-art.
Further improvements in the circulation systems include extended nozzle
bits, seven to twelve nozzles in PDC bits, and the various water courses in
diamond bits.

Thursday, 28 January 2016

Swab And Surge Pressures

Swab And Surge Pressures

Both swab and surge pressures are caused by moving the drillstring axially, and can be calculated using a method similar for calculating annular pressure losses. The greatest difficulty is determining the fluid flow velocity in the annulus when the pipe is opened-ended, because the
distribution of flow between the drillstring and annulus cannot be determined by a simple method.
Two approaches have been proposed.

The first assumes that fluid levels in the annulus and drillstring remain equal at all times. Annular fluid velocity then becomes:


where: Va = Average velocity (ft/min)
Vp = Drillstring velocity (ft/min)
D = Borehole Diameter (inches)
d = Drillstring Outside Diameter (inches)
di = Drillstring Inside Diameter (inches)

The minus sign is in the equation because the drillstring velocity is in the opposite direction to the fluid velocity.

This average velocity equation remains valid even when hole geometry changes. This method is easy to apply and is in widespread use in the oilfield. Its basic premise, that fluid levels in the drillstring and annulus
remain equal, is rarely justified. Because of the greater restrictions to flow, caused by the bit nozzles and pipe bore, actual flow in the annulus will nearly always exceed that calculated by this method. Calculated swab and surge pressures are therefore usually too low.


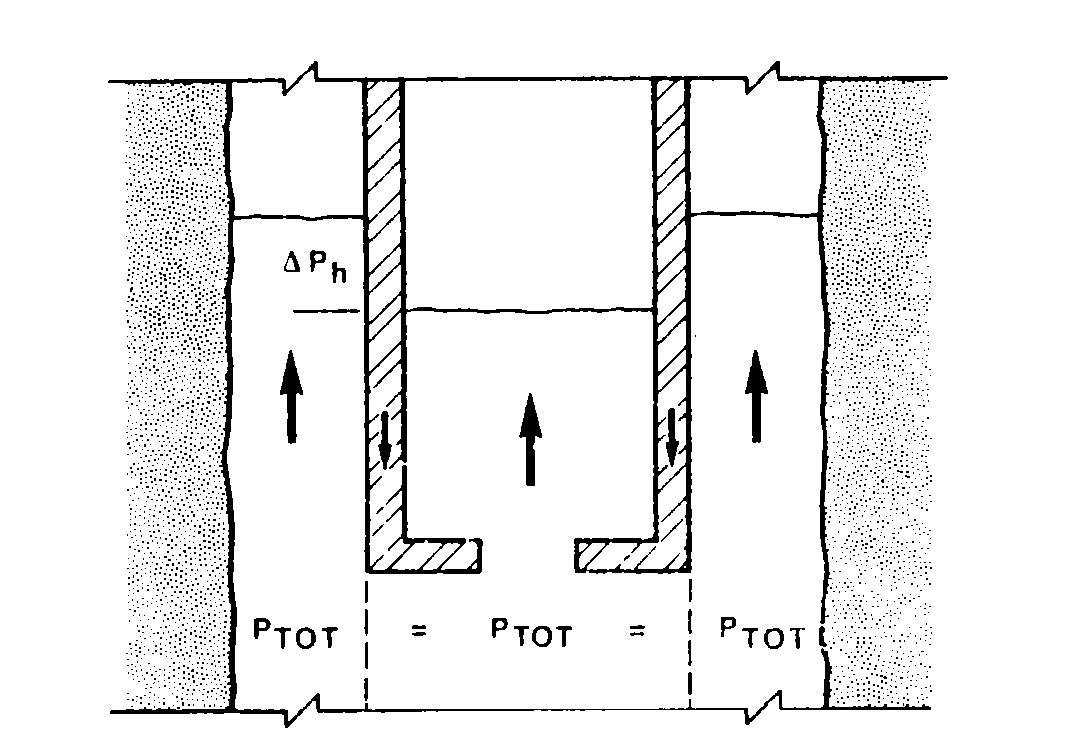
An alternative procedure considers the drillstring and the annulus as a “UTube”, as shown in the following figure.
 It is clear that the sum of hydrostatic and frictional pressures in the pipe bore and through the bit should equal the sum of hydrostatic and frictional pressures in the annulus. Both sums represent the pressure prevailing immediately below the bit.
There is only one flow distribution that will fulfill this criterion, and it can
be found by trial and error through the use of the pressure loss equations.

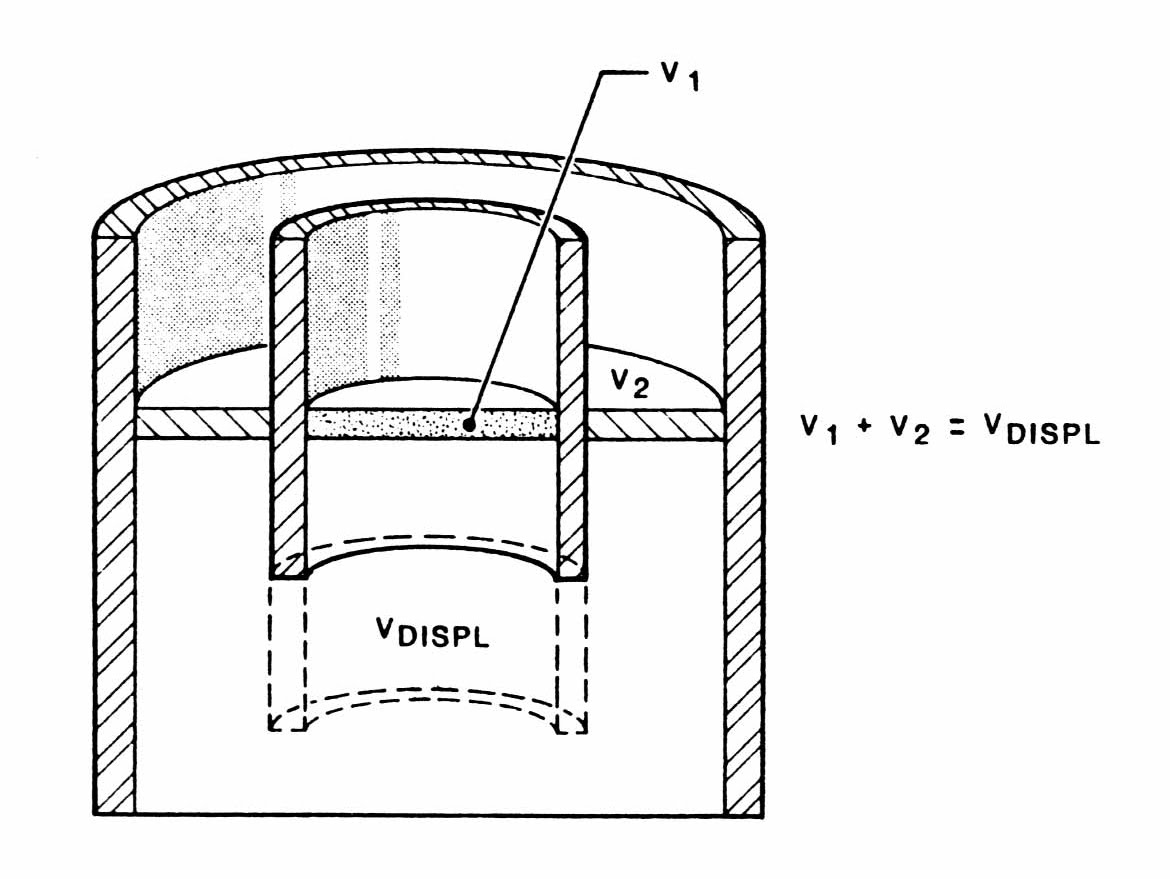
Figure 1-3: Equal Level Displacement

When tripping out of the hole, it may be assumed that both drillstring and annulus are kept full of fluid. The required distribution of flow is that which gives equal frictional losses in the pipe bore and annulus. When tripping into the hole, the fluid level inside the drillstring can drop well below that in the annulus, if small bit nozzles are present. This effect is usually seen as a pit volume being higher than expected, string weight lower than expected, and a considerable volume being pumped before standpipe pressure builds up while breaking circulation.

When the fluid level in the drillstring is below that of the annulus, a greater hydrostatic pressure will exist in the annulus, and fluid will tend to flow from the annulus up the drillstring. In this case, calculating flow distribution by equating frictional losses gives a calculated annular flow and surge pressure slightly higher than actually exists. Because this error is small and conservative, and because at present there is no reliable way of measuring the fluid level within the pipe, the practice of calculating flow distribution by equating internal and external pressure losses is generally accepted.

If the pipe is closed, or contains a float sub, it is easy to calculate flow in the annulus, because all of the fluid displaced by the drillstring passes up the annulus.

Calculating the pressure drop in the annulus is complicated by the motion of the inner wall of the drillstring. This motion is in the opposite direction to the displaced fluid, so the pressure drop will be greater than that for the same flowrate in a stationary annulus . Equations describing the system can be formulated, but solutions are usually too complicated for wellsite use.
Figure
 

Bit Hydraulics And Optimization - Diamond Bit Flow Patterns

Diamond Bit Flow Patterns

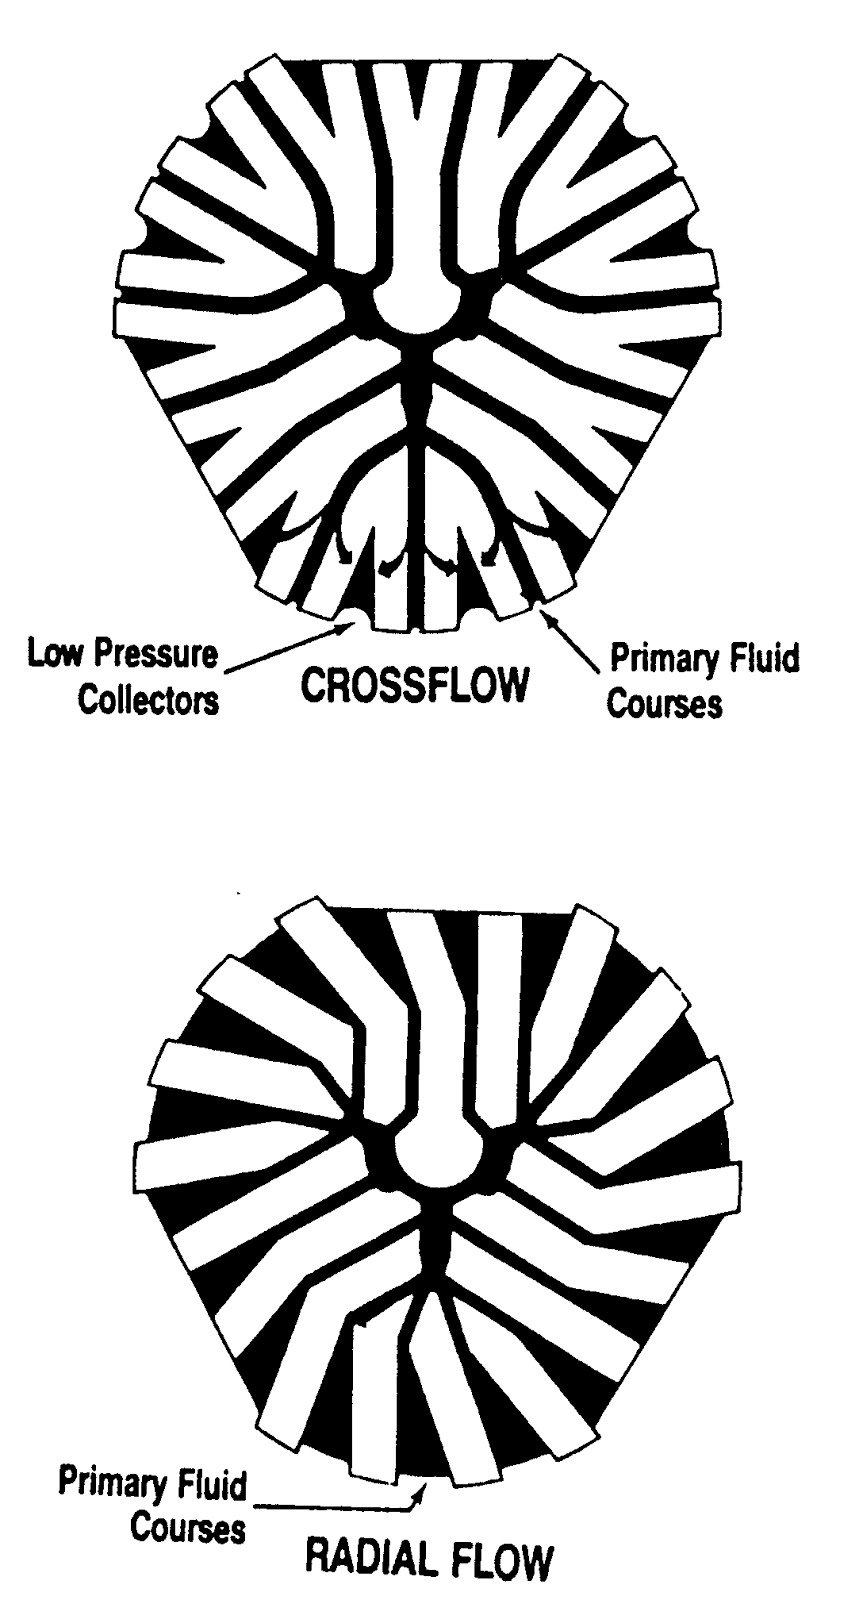
There are two main flow patterns in diamond bits:

1. Cross Pad Flow System (feeder/collector system)

a) the fluid travels along the high pressure “primary fluid courses” (those which connect to the crowfoot), to a point where “low pressure collectors” draw the fluid across the diamond pad
b) this ensures that the diamonds towards the outside diameter are cleaned and cooled
c) The HSI should be between 1.5 and 2.5.

2. Radial Flow System

a) provides a “high pressure primary fluid course” for each diamond row
b) permits fluid to travel in front of, and behind each diamond pad to facilitate cuttings removal and cooling
c) maintains uniform horizontal fluid velocity by tapering fluid course depth as they approach the outside diameter
d) The HSI should be between 2.0 to 3.0.


Bit Hydraulics And Optimization - Diamond Bit Hydraulics

Diamond Bit Hydraulics

The horizontal fluid velocity is the key element in diamond bit life and bit performance. It can be determined using:
The fluid courses assist this by directing the drilling fluid across the bit to cool the diamonds and to remove the cuttings.

 The diamond bit “Total Flow Area” consists of two components:

1. Fluid Course Area - is the area of all fluid courses on the bit. They are cast into the bit body.
2. Diamond Exposure Area - is the area between the bit face and formation, produced by the diamond exposure.

The desired TFA is calculated and designed into the bit by varying the diamond exposure, and the width and depth of the fluid courses. Another phenomenon which occurs with natural diamond bits is called hydraulic pump-off. The hydrodynamic pressure of the mud at the bit acts over the bit face area (between the cutting face of the bit and the formation) and tends to lift the bit off the bottom of the hole. For example, the pumpoff force on a 8-1/2 inch radial flow diamond bit (having a pressure drop of 900 psi) would be approximately 8600 pounds. It will require at least this much bit weight to keep the face of the bit in contact with the bottom of the hole.

Bit Hydraulics And Optimization - PDC Bit Hydraulics

PDC Bit Hydraulics

Since PDC bits are formation specific (best used in plastic formations), the formation characteristics will determine the hydraulic energy required. The drilling fluid will dictate the HSI, for water-based drilling fluids it will be between 2.5 and 4.5, while for oil-based drilling fluids it will be between 1.5 and 3.0.

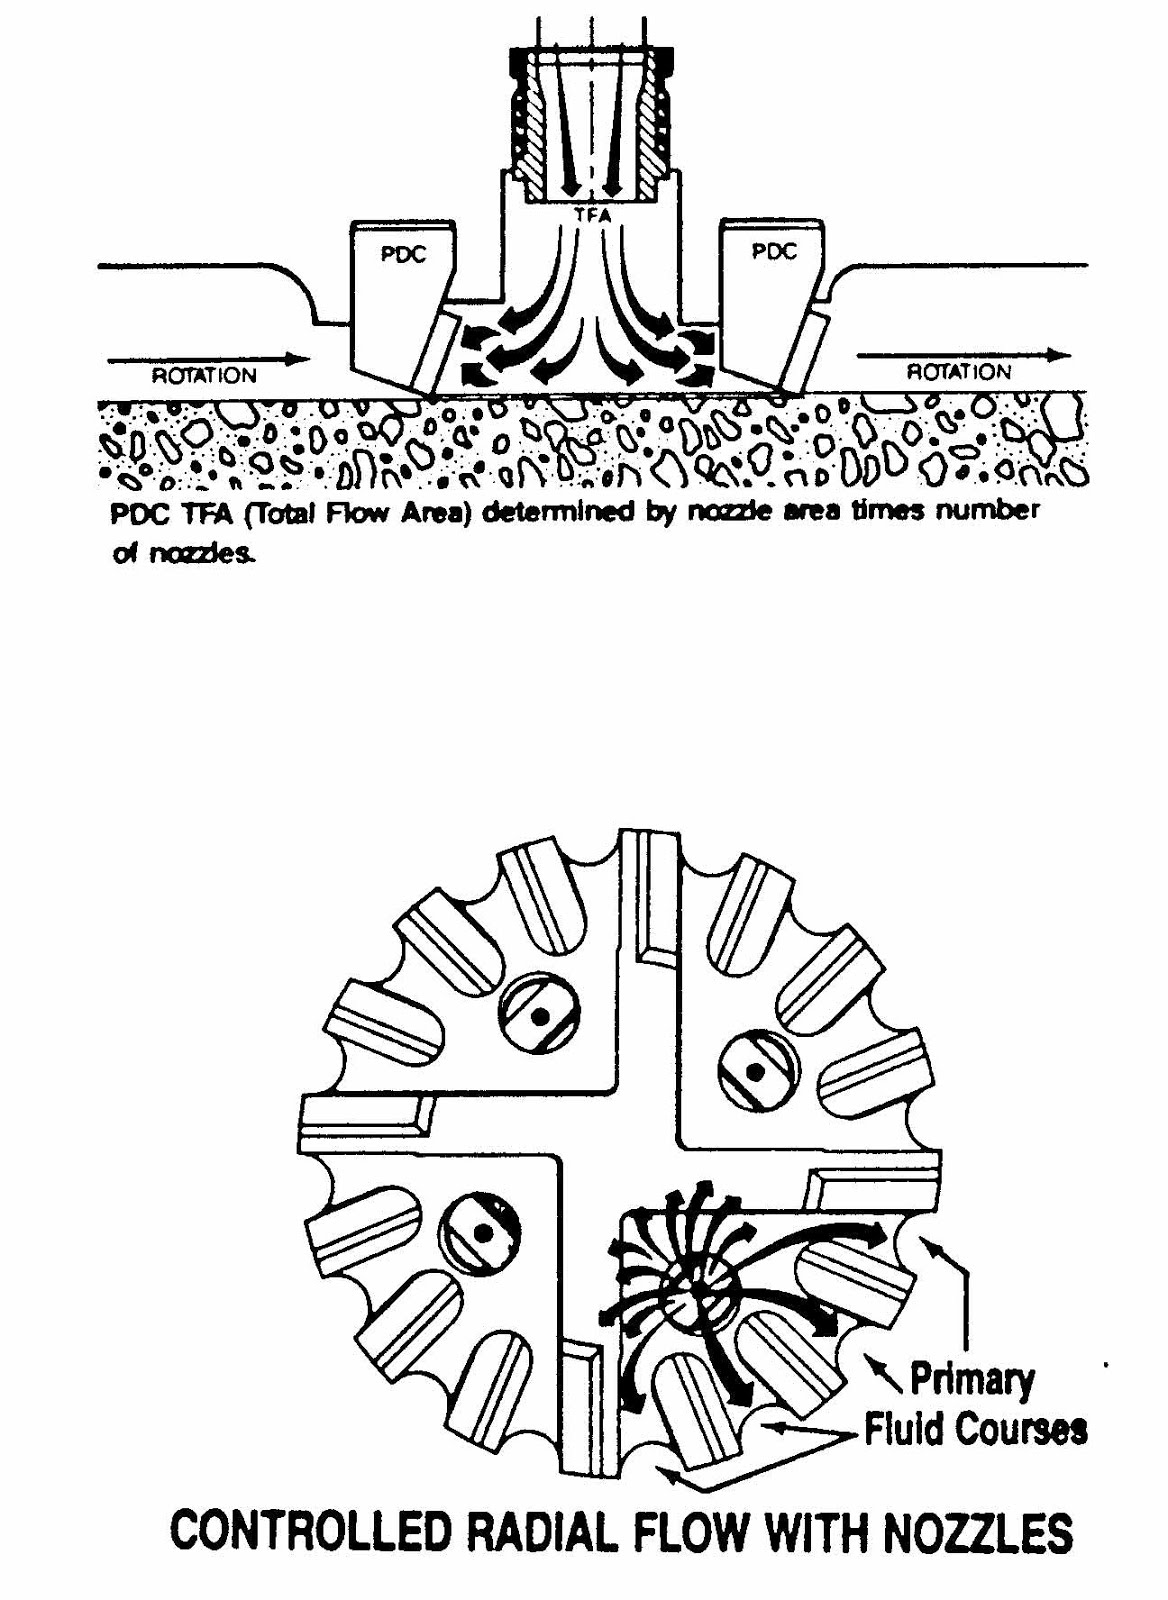
The HSI, calculated at the jet nozzle orifices, will have several characteristics which will directly affect hydraulic energy:

1. the fluid velocity decreases rapidly once it leaves the nozzles
2. high vertical velocity and low horizontal velocities are achieved across the bit face
3. for higher volumes of fluid pumped, horizontal velocities will increase, but not necessarily HSI

The increased horizontal velocities provide better cuttings removal, better cooling, and possibly better drill rates.

Nozzle velocity is calculated in the same manner as with rollercone bits.

Bit Hydraulics And Optimization-Fixed Cutter Bit Hydraulics

Fixed Cutter Bit Hydraulics
The hydraulics for fixed cutter bits is based on the drilling fluids ability to remove cuttings beneath the cutters and to cool the bit. Fluid volume is critical to PDC bit performance. Fluid volume and fluid velocity is critical to diamond bit performance.

The major components of fixed cutter bit hydraulics are:

1. flow rate - Q (gal/min) and V (ft/min)
2. drilling fluid characteristics - MD (lb/gal), YP (lbs/100ft2) and PV (cps)
3. pressure loss - across the bit face (diamond bit) or through the jet nozzles (PDC bit)
4. the Total Flow Area (TFA) - instead of nozzle sizes

A very important parameter in fixed cutter bits is “Hydraulic Power Per Square Inch” or HSI. It is calculated using Hhp (hydraulic horsepower):

where: Hhp = Hydraulic Horsepower
A = Bit Area (square inches)*
* If the area of the bit is not given, it can be calculated using:

where: d = bit diameter (inches)
The hydraulic horsepower equation is the same (Pb x Q/1714), however in fixed cutter bits, resistance to fluid flow is created by the diamonds, nozzles, flow area restrictions, cuttings and the uneven hole pattern. Pressure losses at the bit are calculated using:

Bit Hydraulics And Optimization - Hydraulic Impact Force

Hydraulic Impact Force
Hydraulic (Jet) Impact Force is based on the theory that cuttings are best removed from beneath the bit when the force of the fluid leaving the jet nozzles and striking the bottom of the hole is the greatest. Impact Force is determined by:


where: MD = Mud Density (lb/gal)
Q = Flow Rate (gal/min)
Vn = Nozzle Velocity (ft/sec)
As can be seen, Impact Force depends on maximizing flow rate and nozzle velocity rather than pressure. Therefore, higher flow rates are required. The emphasis is on a large volume of fluid impacting with moderate force, rather than a small volume impacting at a high pressure.
This condition is optimized when circulating rates and bit nozzle sizes are chosen which will cause 48% of the pump pressure to be used to force fluid through the jet nozzles.

Bit Hydraulics And Optimization - Hydraulic Horsepower

Hydraulic Horsepower

Hydraulic horsepower is based on the theory that cuttings are best removed from beneath the bit by delivering the most power to the bottom of the hole. 

The amount of pressure lost at the bit, or bit pressure drop, is essential in determining the hydraulic horsepower. Bit pressure drop is determined by:


where: MD = Mud Density (lb/gal)
Vn = Nozzle Velocity (ft/sec)

From the bit pressure loss, hydraulic horsepower can be calculated:


To optimize Bottom Hole Cleaning and Bit Hydraulic Horsepower, it is necessary to select a circulation rate and nozzle sizes which will cause 65% of the pump pressure to be expended forcing the fluid through the jet nozzles of the bit.   

Wednesday, 27 January 2016

Bit Hydraulics And Optimization - Bottom Hole Horsepower

Bottom Hole Horsepower

Determination of the amount of Bottom Hole Cleaning necessary to maximize the drill rate is based upon:

1. Hydraulic (Jet) Impact Force
2. Hydraulic Horsepower

Maximizing Hpb involves minimizing Hpc, or in other words, the lowest flow rate and the highest pump pressure will result in the highest Hpb. However, the “lowest flow rate” will usually result in inadequate bottom hole cleaning. To compensate for this, bottom hole pressure can be increased by using smaller jet nozzles.

Bit Hydraulics And Optimization - Surface Horsepower

Bit Hydraulics And Optimization- Surface Horsepower


In order to maximize a hydraulics program, all aspects concerning drilling fluids and the associated equipment must be considered. The first component in any hydraulic design is the surface equipment and the hydraulic horsepower available from them. There are two limiting factors on the surface hydraulic horsepower.

The first is the flow rate range. As discussed earlier, the flow pattern in the annulus should be laminar, therefore the upper limit for the flow rate is a Reynolds Number of 2000. The highest velocity in the annulus will be around the collars, and this velocity can be determined by calculating the “critical velocity” over that section. In addition, running the pumps at that upper range is not always advisable because there will be more wear and tear on the pumps and much more fuel consumption.

The lower limit is a range where there is sufficient hole cleaning. This is determined by using the velocity around the drillpipe and the largest annular section (normally the upper hole section or drillpipe/riser section). 

A normal range is around 50 ft/min.
The second factor is the operating pressure of the mud pumps. Most mud pumps can produce the required pressure with little problem. However, because of the various components associated with the surface system (standpipe, rotary hose, pulsation dampener, etc.) the maximum surface pressure is usually limited to some value less than the maximum rated pump pressure.

The available “surface horsepower” is then determined by:


where: Hps = Surface Horsepower
P = Pump Pressure (psi)
Q = Pump Flow Rate (gal/min)
Once the surface horsepower has been determined, the horsepower distributions can be made:


where: Hpc = Circulation Horsepower
Hpb = Bit Horsepower